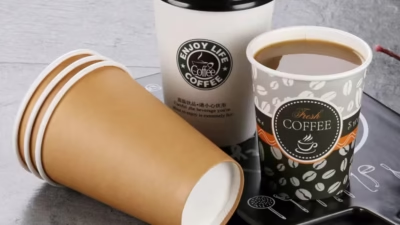
Single-wall paper cups remain everyday items found in coffee shops, offices,s and local diners across town. People grab these lightweight vessels daily for morning espresso or afternoon tea during busy commutes. Simple manufacturing processes allow makers to roll thin paper sheets into functional cylinders with bonded bottom disks.
Businesses often buy custom single wall paper cups to display brand logos directly to consumers walking down busy streets. Finding reliable production partners helps shop owners maintain steady inventories without running short during peak morning rushes.
Material Selection Basics
Choosing the right paper stock ensures hot liquids stay contained without weakening the outer container walls during use. Manufacturers use food-grade paperboard coated with thin polyethylene layers to prevent moisture leakage onto wooden tables or hands. Selecting sturdy materials prevents container collapse when customers squeeze cups tightly while walking outside in cold weather. Purchasing 8oz single wall paper cups gives buyers a standard capacity ideal for serving regular portions of black coffee or herbal tea. Suppliers test raw materials rigorously to guarantee safety standards match strict food contact regulations worldwide.
Bulk Purchasing Methods
Ordering commercial supplies in large quantities reduces overall operational expenses for growing beverage businesses managing tight monthly budgets. Warehouses stock large inventories of single wall paper cups in bulk to ensure cafes never run out during unexpected customer surges. Wholesale buyers examine pallet pricing structures carefully before signing long term contracts with industrial container distributors. Management teams calculate storage space requirements inside stockrooms prior to scheduling massive delivery trucks carrying thousands of nested beverage vessels. Bulk acquisition strategies help independent coffee house owners compete effectively against large international franchise chains operating nearby.
Manufacturing Supply Chains
Industrial factories utilize high-speed machinery to cut and seal paper components into finished beverage containers efficiently. Verified single-wall paper cup suppliers maintain strict quality control protocols throughout every stage of automated production lines. Technicians monitor adhesive application and seam integrity continuously to eliminate defective units before packaging items for global distribution. Global logistics networks connect raw material mills directly with packaging assembly plants located across major industrial trade zones. Factory managers prioritize eco-friendly production methods to minimize waste and reduce environmental impacts associated with disposable paper goods.
Brand Customization Techniques
Printing company logos onto beverage containers transforms ordinary disposable items into mobile advertisements moving through urban environments daily. Coffee shop owners commission custom single-wall cups featuring unique brand artwork to build strong visual recognition among local buyers. Graphic designers adjust color profiles carefully so printed graphics appear sharp and vibrant against white or brown paper backgrounds. Specialized printing presses apply food-safe inks that withstand heat from boiling water without fading or transferring chemical odors. Brand promotion through branded drinkware remains a cost-effective marketing strategy for independent cafes seeking customer loyalty.
Production Industry Standards
Industrial fabrication facilities adhere to strict international guidelines to ensure disposable paper items meet consumer safety expectations completely. Qualified single-wall paper cup manufacturers invest heavily in modern technology to improve operational speed and reduce energy consumption. Factory inspectors check raw paper thickness and base seal strength randomly during active shifts to maintain high-quality output. Environmental compliance audits evaluate factory waste management systems regularly to ensure sustainable practices guide daily manufacturing operations. Adhering to recognized industry standards builds long term trust between packaging producers and commercial beverage vendors worldwide.
Corporate Logo Printing
Adding corporate emblems to takeaway drinkware creates professional impressions during business meetings and outdoor promotional community events alike. Organizations order custom 8oz single wall paper cups with logo prints to showcase company branding at large-scale gatherings. Marketing coordinators coordinate closely with printing technicians to match exact corporate color guidelines onto curved paper surfaces. High-resolution printing equipment captures fine details accurately, ensuring text remains legible even on smaller cup circumferences. Branded drinkware enhances corporate identity visibility while providing practical utility during catered breakfast seminars and office functions.
Commercial Distribution Networks
Efficient shipping systems move packaged beverage containers from manufacturing plants to regional distribution warehouses without unnecessary logistical delays. Local distributors offer Single Wall Paper Cups Wholesale purchasing options designed specifically for small business owners and independent shop operators. Inventory managers track stock levels using digital software platforms to prevent out-of-stock situations during seasonal demand peaks. Transport fleets utilize optimized routing schedules to deliver fragile paper goods safely to retail store loading docks on time. Strong distribution partnerships ensure continuous supply chain reliability for commercial enterprises relying on steady packaging deliveries.
Conclusion
Single-wall paper cups continue serving essential roles within the modern food service industry by offering convenient beverage containment solutions. Understanding manufacturing methods, material grades, and purchasing options helps business owners make informed decisions regarding operational supplies. Selecting reliable production partners ensures consistent product quality and steady inventory levels throughout busy operating seasons. Careful planning regarding container selection contributes directly to smooth daily cafe operations and positive customer satisfaction outcomes everywhere.erywhere.